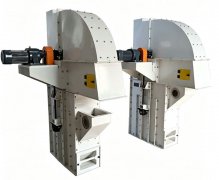
Heavy-Duty Bucket Elevator
It is engineered for continuous, high-capacity vertical lifting of bulk, abrasive, and heavy materials in extreme industrial environments from low to high levels. The price range is $2,500-$15,000.
Traction Type: Heavy-duty steel cord belts or forged alloy steel chains
Max. Feed Size: 25-70 mm
Conveying Capacity: 6.5–160 T/H
Lifting Speed: 1.4–2.0 m/s
Max. Lifting Height: ≤ 65 meters (customizable)
Application Range: Cement, mining, aggregates, and chemical processing plants
Our heavy-duty bucket elevator is engineered for continuous, high-capacity vertical lifting of bulk, abrasive, and heavy materials in extreme industrial environments. Designed to withstand rigorous daily operations, it ensures reliable performance and maximum throughput for demanding processing plants.
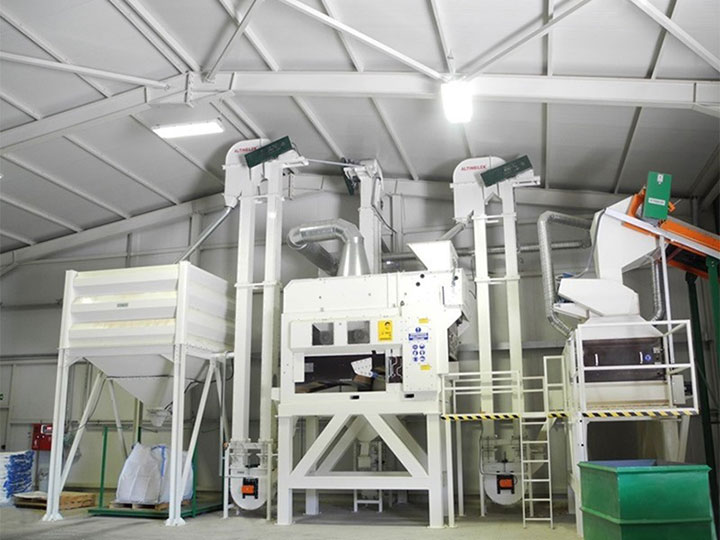
Overview & Core Advantages of Our Heavy-Duty Bucket Elevator
- High-Capacity Throughput: Optimized bucket spacing and high-speed driving options deliver massive vertical material elevation.
- Extreme Durability: Built with heavy-gauge reinforced casing and wear-resistant components to handle harsh minerals and aggregates.
- Anti-Clogging Design: Streamlined material inlet and discharge dynamics prevent material accumulation and bucket blockages.
- Reliable Safety Protection: Integrated with heavy-duty backstops and robust tensioning systems to ensure secure, continuous operation.
Product Series & Types
Our heavy-duty bucket elevators are available in two primary configurations to match different operational demands:
- Belt-Type Heavy-Duty Bucket Elevator: Ideal for high-speed, high-capacity, and quieter continuous vertical lifting.
- Chain-Type Heavy-Duty Bucket Elevator: Built with forged alloy steel chains for extremely heavy, abrasive, or high-temperature bulk materials.
Technical Specifications & Model Selection Matrix
Review our heavy-duty bucket elevator model specifications below. Custom heights and configurations are available upon request to fit your exact plant layout.
| Model | Max. Feed Size (mm) | Capacity (T/H) | Lifting Speed (m/s) | Belt / Chain Width (mm) | Max. Lifting Height (m) |
|---|---|---|---|---|---|
| HD160 | 25 | 6.5 – 18 | 1.4 | 200 | ≤ 45 |
| HD250 | 35 | 14 – 40 | 1.6 | 300 | ≤ 45 |
| HD315 | 45 | 20 – 48 | 1.6 | 400 | ≤ 50 |
| HD400 | 55 | 28 – 75 | 1.8 | 500 | ≤ 55 |
| HD500 | 60 | 45 – 110 | 1.8 | 600 | ≤ 60 |
| HD600 | 70 | 95 – 160 | 2.0 | 700 | ≤ 65 |
Key Structural Features & Engineering Highlights
Our heavy-duty bucket elevator incorporates robust engineering principles to ensure maximum reliability, minimal maintenance, and long service life in harsh operating conditions.
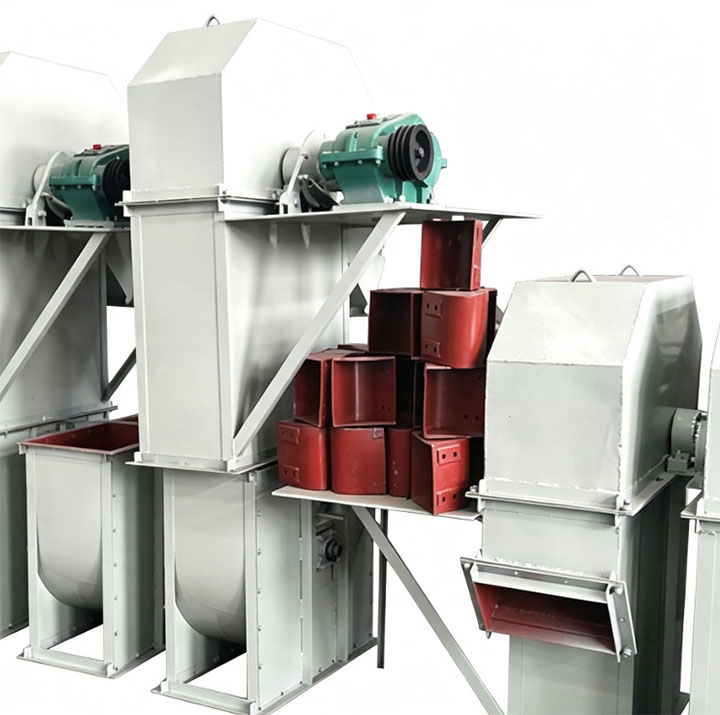
- High-Tensile Traction Components: Equipped with heavy-duty steel cord belts or forged alloy steel chains, engineered to handle extreme tensile loads over high vertical lifts without stretching.
- Wear-Resistant Buckets: Fabricated from high-grade abrasion-resistant steel or reinforced polymer, featuring thickened lips to resist impact and wear from coarse, heavy minerals.
- Integrated Safety Protection: Designed with heavy-duty backstops to prevent reverse rotation during power outages, alongside optional sensors for speed monitoring, belt misalignment, and bearing temperature.
Typical Applications in Heavy Industries
Engineered for continuous vertical transport, our heavy-duty bucket elevator is widely implemented across demanding industrial sectors for handling bulk solids:
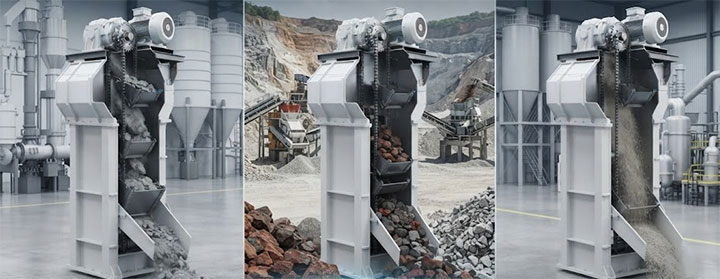
- Cement & Building Materials: Ideal for vertical elevation of raw meal, cement clinker, limestone, and gypsum, especially within vertical roller mill systems.
- Mining & Aggregates: Designed to withstand heavy abrasive workloads when transporting iron ore, crushed stone, sand, and metallic mineral powders.
- Power & Chemical Processing: Reliable handling of high-capacity bulk materials including fly ash, desulfurization gypsum, and various chemical raw materials.
Frequently Asked Questions (FAQ) on Heavy-Duty Bucket Elevators
How do I choose between a belt-type and a chain-type heavy-duty bucket elevator?
Belt-type elevators are generally preferred for higher speeds, quieter operation, and lighter-to-medium bulk materials. Chain-type are engineered for extremely heavy, abrasive, or higher-temperature materials that require maximum tensile strength and durability over prolonged operations.
What design features prevent material back-spill and bucket clogging?
Our heavy-duty bucket elevators utilize optimized bucket spacing, streamlined casing profiles, and precise discharge dynamics. These elements ensure clean material release at the head section, minimizing back-spill and preventing material accumulation during high-capacity runs.
What is the maximum material temperature this heavy-duty series can handle?
Standard configurations handle materials up to 80°C. However, with optional heat-resistant rubber belts, special chain assemblies, and thermal-insulated casings, our heavy-duty models can safely process high-temperature materials up to 250°C (such as cement clinker).
Tailored Customization & Engineering Support
We understand that every industrial plant has unique spatial and operational constraints. Our engineering team provides comprehensive support from concept to deployment:
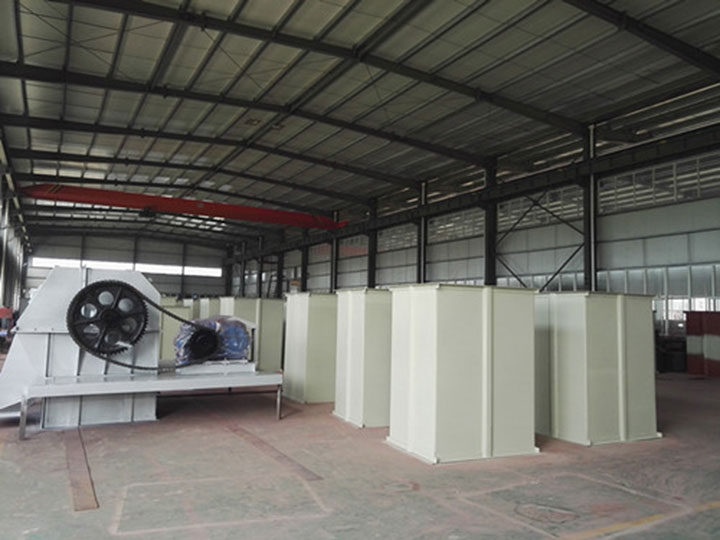
- We tailor lifting heights, inlet/outlet orientations, drive configurations, and material selections to seamlessly match your existing plant layout.
- From professional installation guidance and on-site commissioning to a reliable supply of replacement parts (buckets, chains, belts), we ensure continuous, worry-free operation.
Need a custom solution or a quote for your project?
Contact our engineering experts today to discuss your specific heavy-duty material handling requirement.
Products
Hot Modules
locations


headquarters
Address:China,Yanjin county forest park gate to the west 1000 meters north road.