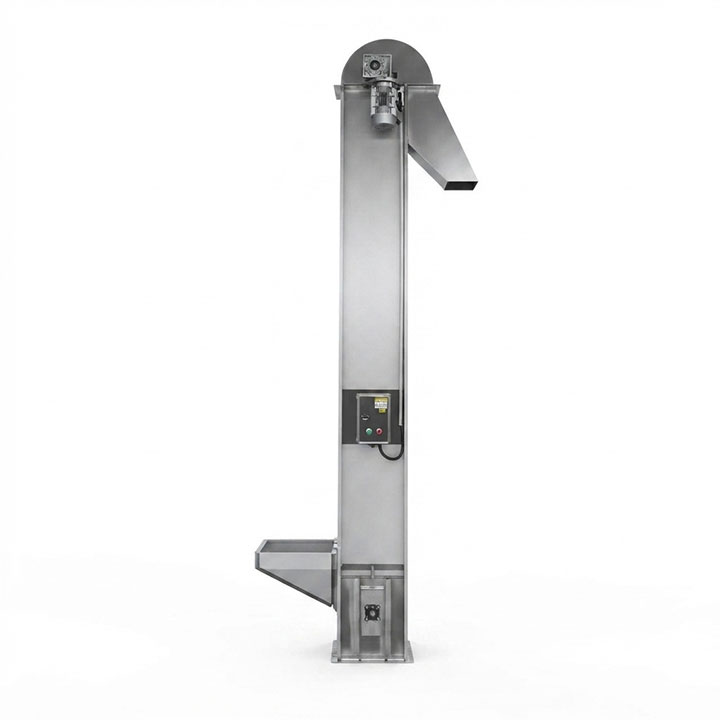
Bulk Material Vertical Elevator
It is an essential industrial mechanism used to transport powdery, granular, and lumpy materials vertically. Our factory provides reliable vertical elevator configurations for continuous operation, minimal maintenance, and dust-tight performance across various processing lines.
| Lifting height | 3-50+ meters |
| Handling capacity | 10-300+ m³/h |
| Power | Customized based on throughput and height |
| Material type | Powdery, granular, and lumpy materials (grains, cement, ores, powders, etc.) |
| Casing/Bucket Material | Carbon steel with anti-corrosive paint, stainless steel (SUS304 / SUS316L), or wear-resistant alloy sheets |
What is a Bulk Material Vertical Elevator?
A bulk material vertical elevator is a heavy-duty industrial lifting machine designed for the continuous, dust-tight vertical transportation of powdery, granular, and lumpy materials. By utilizing precision-engineered traction systems and sturdy casings, it maximizes plant throughput while effectively preventing material degradation and environmental contamination.
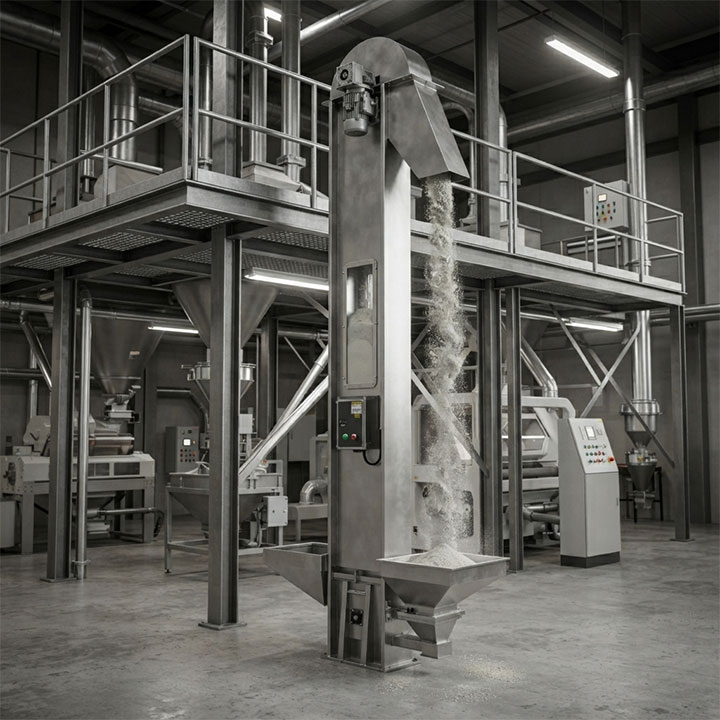
Core Types of Bulk Material Vertical Elevators
Different industrial applications require specific mechanical structures to achieve optimal lifting efficiency. We provide several primary types of bulk material vertical elevators tailored to your material characteristics:
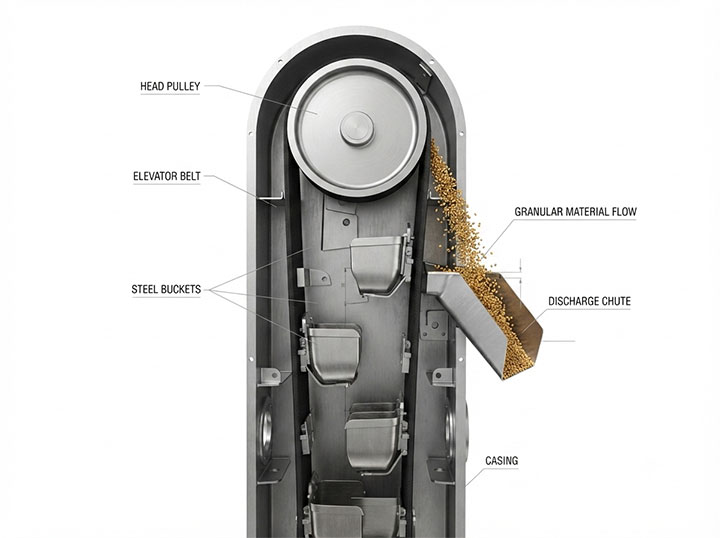 |
Centrifugal Discharge ElevatorsBest suited for free-flowing granular materials like grains and seeds, utilizing centrifugal force for clean discharge into the chute.
|
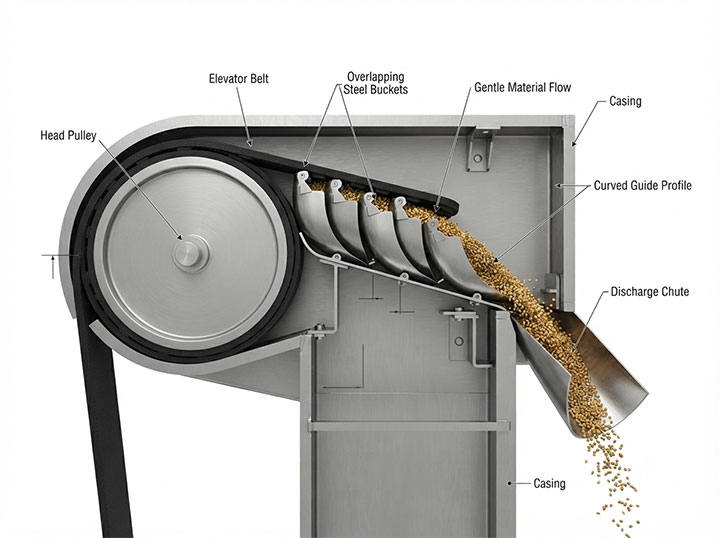 |
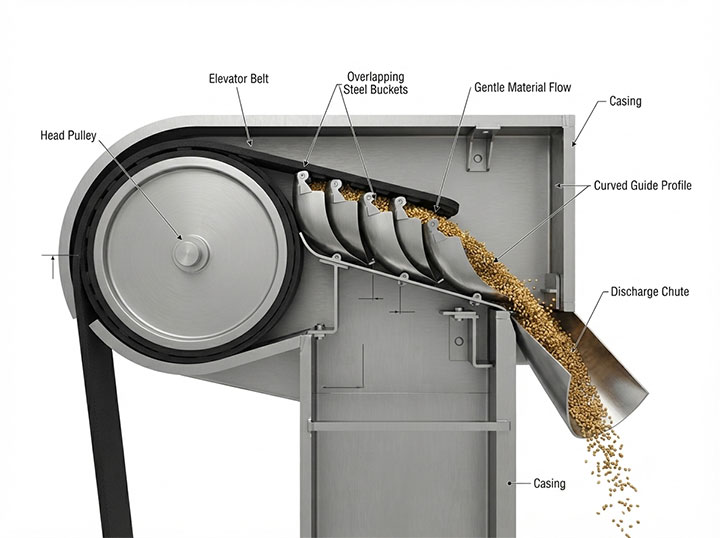
Continuous Discharge ElevatorsDesigned for fragile or aerated powders, operating at lower speeds to prevent material breakage and dusting.
|
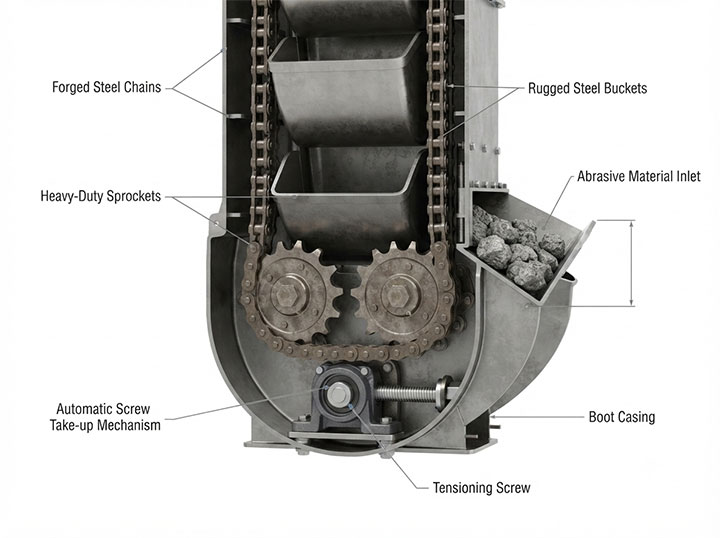 |
Chain-Type Heavy-Duty ElevatorsEngineered with robust chain links to handle heavy, abrasive, and lumpy materials such as cement, ores, and clinker.
|
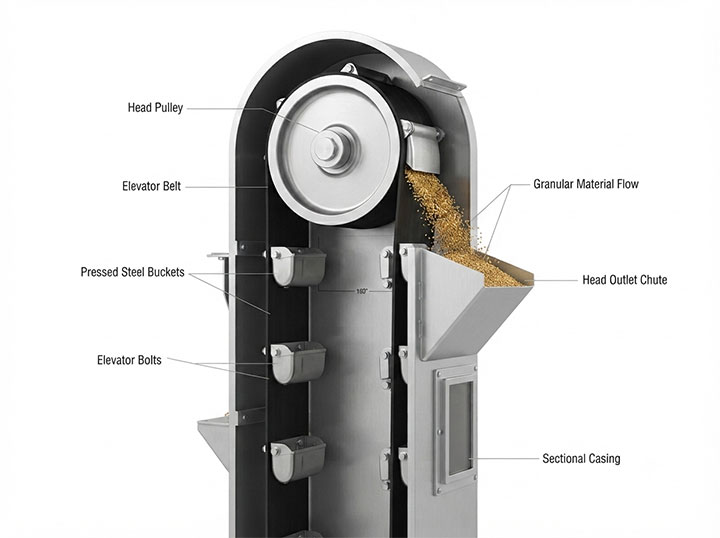 |
Belt-Type ElevatorsOffers cost-effective, high-speed vertical transportation for lighter bulk goods with lower noise emissions.
|
How Our Elevators Handle Tough Bulk Solids
Handling bulk solids requires precise matching between material physical behavior and machine design. Our vertical elevator systems are engineered to address specific material challenges:
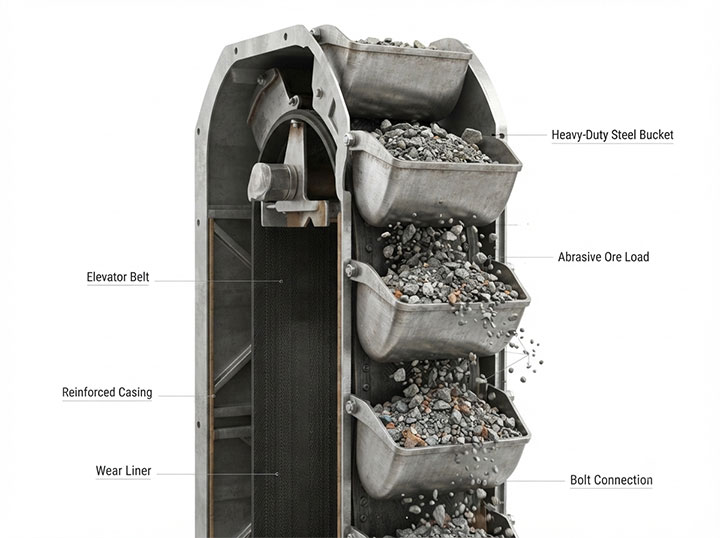
- Abrasive & Heavy Ores: Equipped with wear-resistant steel buckets and reinforced casings to withstand high-impact friction from mineral powders and aggregates.
- Fragile Grains & Seeds: Utilizes low-speed continuous operation and smooth bucket profiles to minimize particle degradation and crop damage during lifting.
- Fine & Dusty Powders: Features fully sealed, dust-tight housing joints and optional flexible connections to prevent material leakage and environmental contamination.
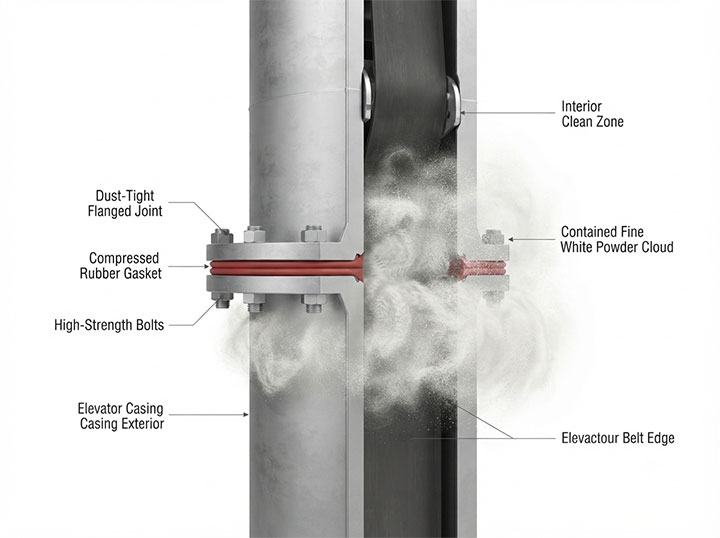
Proprietary Structural Advantages & Mechanical Reliability
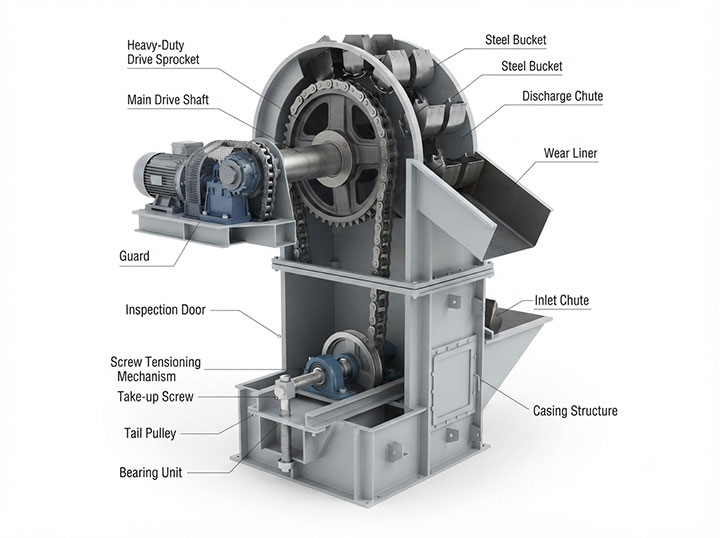
Dahan bulk material vertical elevators integrate precision engineering to ensure long-term mechanical stability and reduce unexpected downtime on your production floor:
- Optimized Drive & Tensioning System: Features a robust bottom-mounted gravity take-up or screw tensioning mechanism to maintain proper belt or chain tension automatically.
- Wear-Resistant Bucket Design: Buckets are fabricated with reinforced lips and high-grade materials to extend service life when handling harsh, abrasive industrial materials.
- Rigid Casing Construction: Precision-welded sectional casings prevent structural twisting and ensure absolute alignment between the head and boot sections.
Technical Specifications & Custom Engineering Parameters
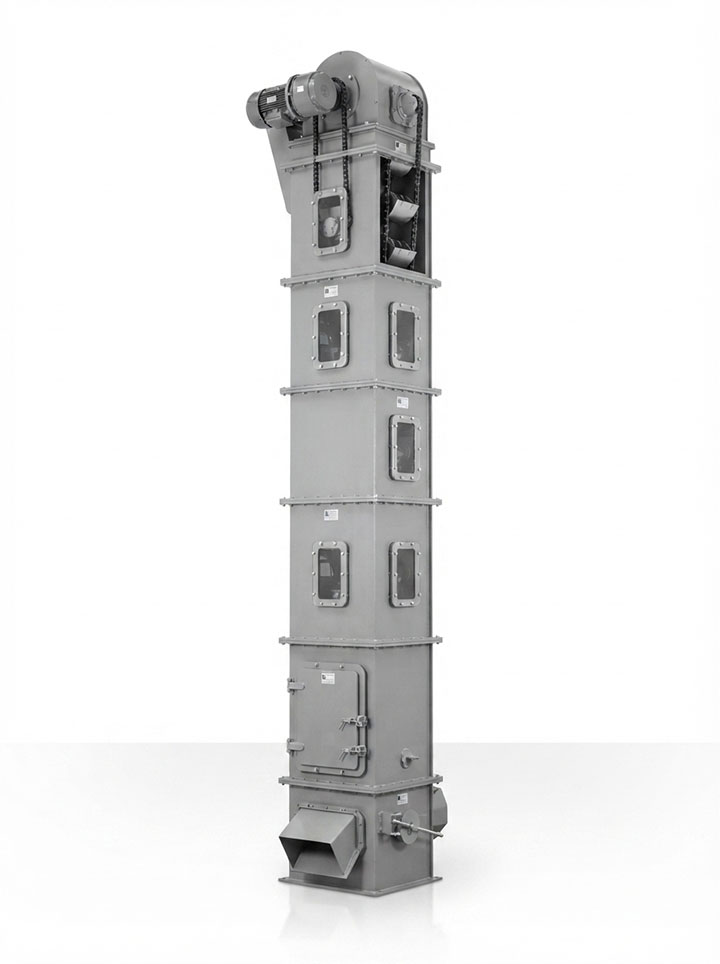
To integrate smoothly into your existing plant layout, our bulk material vertical elevators can be fully customized across key operational parameters:
- Lifting Height: Customized from 3 meters up to 50+ meters based on your vertical workspace requirements.
- Handling Capacity: Ranging from 10 m³/h to over 300 m³/h to match varying plant throughput demands.
- Casing Materials: Available in carbon steel with anti-corrosive paint, stainless steel (SUS304 / SUS316L), or wear-resistant alloy sheets.
- Drive Options: Integrated gear motor assemblies with backstop devices to prevent reverse running during power interruptions.
Proven Field Performance: Industrial Applications in Action
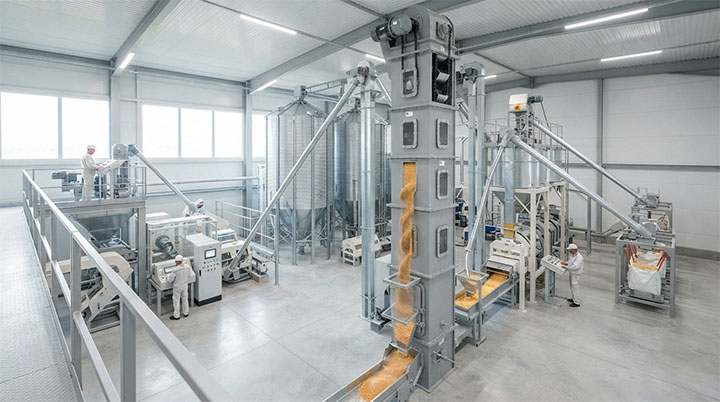
Our bulk material vertical elevators are deployed globally across diverse processing industries, delivering consistent and reliable vertical handling performance. Explore our project records in our Customer Case section to see how our equipment operates in real-world environments:
- Cement & Construction: Efficiently lifting raw meal, clinker, and dry mortar mixes in high-demand production lines.
- Agriculture & Grain: Handling large volumes of wheat, corn, and fertilizer with high throughput and gentle transfer.
- Mining & Metallurgy: Transporting crushed ores, coal powder, and mineral aggregates under heavy-duty conditions.
Our Manufacturing Excellence and Inventory Capacity
We prioritize rigorous quality control and high-standard manufacturing processes for every bucket elevator we produce. The following footage provides a glimpse of our production facility and ready-to-ship inventory, demonstrating our capacity to support large-scale industrial projects with reliable, precision-engineered equipment.
Frequently Asked Questions by Plant Engineers & Procurement Managers
How do you prevent belt or chain slipping and material build-up in high-capacity vertical lifts?
Our elevators feature precision-engineered bottom tensioning mechanisms and self-cleaning boot designs that maintain optimal traction and prevent material accumulation over long operational cycles.
Can the bucket material and casing be customized for corrosive or food-grade applications?
Yes. We offer full stainless steel (SUS304 or SUS316L) construction and food-grade compliant components to meet strict sanitation and chemical resistance standards.
What is the typical lead time for a customized bulk material vertical elevator?
Standard production generally takes 15 to 25 working days. For heavily customized or large-scale multi-unit orders, our engineering team provides a detailed delivery schedule upon project confirmation.
Request a Custom Quote & Engineering Proposal
Ready to upgrade your material handling line? Share your project specifications with us, and our engineering team will provide a tailored technical proposal, detailed drawings, and competitive pricing.
Get in touch directly:
- Email: sale@xxdahan.com
- WhatsApp: +86 18339211009
Or send us your required capacity, lifting height, and material type to receive a prompt solution matching your exact plant requirements.
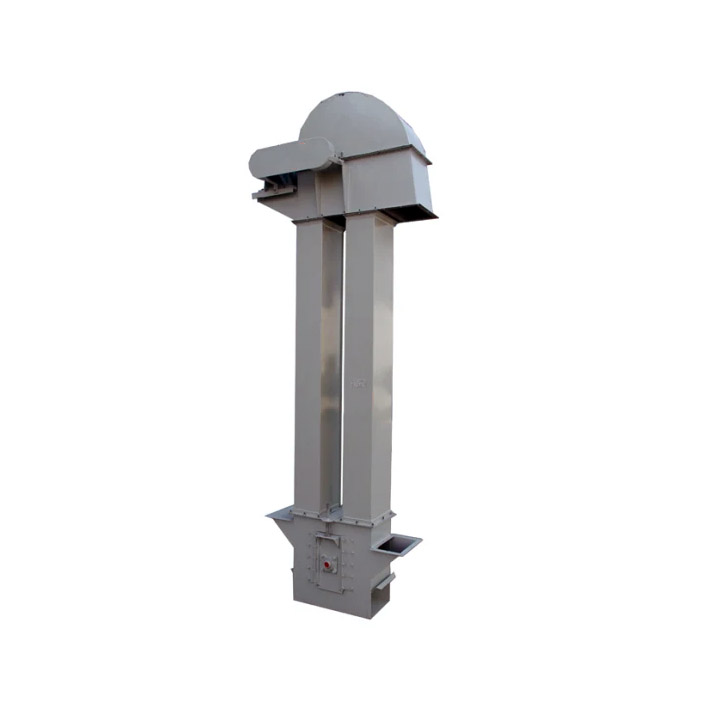 Small Bucket Elevator
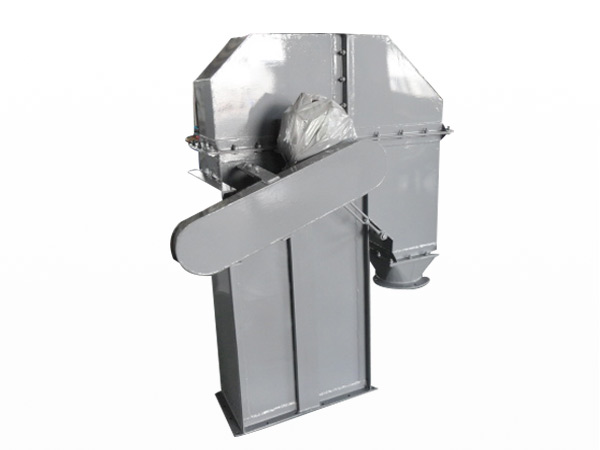 Bucket Conveyor For Sale
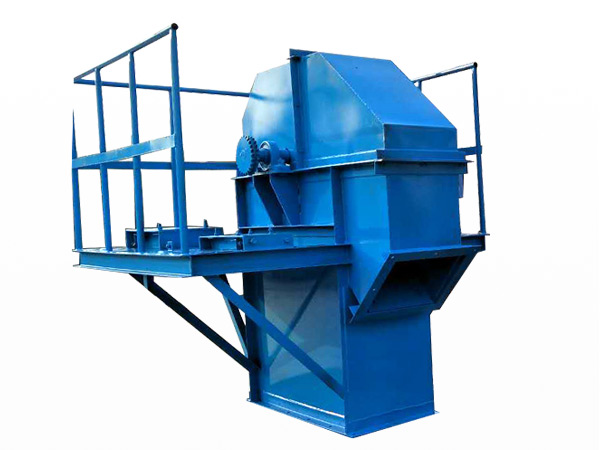 Chain Type Bucket Elevator
Products
Hot Modules
locations


headquarters
Address:China,Yanjin county forest park gate to the west 1000 meters north road.